

For 3Dwork we have spent more than two years working with Lychee Slicer as official partners. We have watched it grow from a promising slicer into what is today the most complete software for resin printing.

This guide is not a summary of the official documentation. It covers what you need to get the most out of Lychee, from the first install to the settings that make the difference between a perfect print and a failed one.
Do you have questions about this electronics? Join our community: Instagram, YouTube, TikTok. And on Telegram: general group 3Dwork, specific group Lychee that we recently created… all of them in Spanish.
What is Lychee Slicer?
Lychee Slicer is a slicing software (slicer) for resin and FDM printers, developed by the team at Mango3D. It turns your 3D models into files the printer can run layer by layer, controlling every UV exposure. The current version is v8.0.3, available for Windows, macOS and Linux.
Unlike most slicers focused on resin, Lychee also works with FDM printers, which makes it a unique environment for anyone who works with both technologies.
But its main strength is still resin: it has tools such as the suction cup detector, the 3D check for drain holes, or the community resin profiles, already calibrated and ready to use with small adjustments for our setup.
Lychee in 2026: what’s new
According to the manufacturer, Lychee Slicer 8 is the biggest release to date. The program leaves Electron behind and gets its own engine. These are the changes you will notice most day to day (official changelog 8.0.0, 24/09/2026):
| Feature | New in v8.0 |
|---|---|
| Engine | Rebuilt: Electron is gone. Interface on Chromium Embedded 150 and rendering on its own Vulkan engine |
| Performance (manufacturer figures, identical scenes Lychee 7 vs 8) | 22× less load when preparing files; 8.4× manual supports; 8.7× model navigation; 6.7× automatic supports; 7× bridges and grids |
| Auto-orientation | Minimises overhanging area and returns the same orientation for the same model. Also in the free version |
| Assembly Keys | Generates pegs and sockets inside the program to join split pieces |
| Editable hollowing | Tube-style brush to edit cavities behind the surface, with footprint in mm |
| Internal supports | Inside hollow cavities and under internal overhangs (interior, exterior or both) |
| Hollowing grid | About 118 MB down to 6 MB on a dense test model (grid only, not total memory) |
| Mesh repair | Rewritten algorithm for more reliable fixes on complex or damaged meshes |
| .lys files | No longer freezes when opening projects with missing files: it tries to recover the backup or says what is missing |
| Printer connection | New base for TCP, UDP, Wi-Fi and serial. Chitu cameras restored |
| Formats | Multi-object 3MF (Production Extension) and Goo v5 for Anycubic Jupiter 2 |
| Licences | Go from two to three seats |
Lite, Plus and Library: which one you need
This is the question we get in every resin printer review. The honest answer: the Lite version is enough to start and for 60% of users. The step up to Plus is worth it if you print regularly or need the ML Auto-Supports.
| Feature | Lite (Free) | Plus (€9.99/month) | Plus & Library (€19.99/month) |
|---|---|---|---|
| Basic slicing | ✅ | ✅ | ✅ |
| Manual supports | ✅ | ✅ | ✅ |
| Island detection | ✅ | ✅ | ✅ |
| Anti-aliasing | ✅ | ✅ | ✅ |
| Community profiles | ✅ | ✅ | ✅ |
| Basic hollow | ✅ | ✅ | ✅ |
| ML Auto-Supports | ❌ | ✅ | ✅ |
| Suction Cup Detector | ❌ | ✅ | ✅ |
| Hollow 3D + blockers | ❌ | ✅ | ✅ |
| Full multiplate | Limited | ✅ | ✅ |
| Support painting | ❌ | ✅ | ✅ |
| Grid & Projection support | ❌ | ✅ | ✅ |
| Pre-supported models (2,500+) | ❌ | ❌ | ✅ 120+ libraries |
| Annual price | Free | €99.90/year | €199.90/year |
How to download and install Lychee Slicer
The official download is at mango3d.io/downloads. The current version is v8.0.3. Available for Windows, macOS and Linux (Deb + AppImage).
- 🔗 Download Lychee Slicer 8.0.3 — free Lite, with a 30-day Plus trial included
- 📚 Lychee Academy — free official tutorials to learn at your own pace
- 💬 Discord Mango3D — community of more than 29,000 members with real-time help
Step 1: Download the Windows installer from mango3d.io/downloads and run it. If Windows shows “Windows protected your PC”, click “More info” → “Run anyway”. It is a generic warning for unsigned software from Microsoft. It does not indicate a risk.
Step 2: Accept the licence agreement. Lite is completely free for personal and commercial use.
Step 3: Choose the installation folder. The default path works perfectly.
Step 4: The installer copies the files. It takes 1–3 minutes. Lychee updates automatically: when a new version is available, it notifies you on startup.
Step 5: Installation complete. When you open Lychee for the first time, the 30-day free Plus trial activates automatically. Use it to explore the Auto-Supports and the Suction Cup Detector before deciding whether to subscribe.
Download the .dmg, open it and drag Lychee into the Applications folder. No install wizard.
If macOS says it cannot verify the developer: System Settings → Privacy & Security → Open Anyway. You only need to do this the first time.
Linux: Available as .deb (Ubuntu/Debian) or .AppImage (any distro). The AppImage is portable and needs no installation: download it, give it execute permission and you are done.
System requirements
| Minimum | Recommended | |
|---|---|---|
| CPU | Intel i5 / AMD Ryzen 5 | Intel i7 / AMD Ryzen 7 (or Apple M1 Pro) |
| RAM | 16 GB | 32 GB or more |
| GPU | GTX 960 / RX 580 (1 GB VRAM) | RTX 3060+ / RX 6700+ (4 GB VRAM) |
| Storage | 10 GB free | SSD with 20+ GB |
| Screen | 1280×800 | 1920×1080 or higher |
| OS | Windows 10 64-bit / macOS / Ubuntu | Windows 10/11 64-bit or macOS with M1+ |
First setup: printer and resin profile
The first time you open Lychee, the setup wizard asks you to configure your printer and your resin. These two settings define everything else: build volume, resolution and starting exposure times. If these two are not set correctly, nothing will work well.
Adding your printer
- Click “Add Printer” in the right-hand panel.
- Search for your model in the search field (e.g. “Elegoo Saturn 4”) or browse by brand.
- Select the exact model — check the screen resolution number to confirm it is yours.
- Lychee loads the official profile with the base values validated by the manufacturer.

Setting up the resin profile
Once you have the printer, the next step is to select the resin you are going to use. This is where Lychee has a clear advantage over other slicers: the Community Resin Profiles.

- Click “Add Resin” in the settings panel.
- Search for your resin by name (e.g. “Elegoo ABS-Like Grey”).
- If a community profile exists for your printer + resin combination, use it as a starting point — someone with your same setup has calibrated it.
- If none exists, enter the manufacturer’s values and calibrate with an exposure test (see below).
The Lychee Slicer interface explained

The interface is organised into logical zones. Once you know them, the workflow becomes very fast:
- Left panel: main tools — import models, supports, hollowing, cutting and measuring tools.
- Central viewport (3D view): this is where you handle the model. Right click to rotate the camera, scroll wheel to zoom, middle click to pan.
- Right panel — Printer: active printer selector and resin settings.
- Right panel — Settings: all the slicing parameters. The most important one.
- Bottom bar: plate information — estimated time, resin volume, number of layers.
- Slice + Preview button: slice and review layer by layer with the Picture View and Slice View viewers.
Display modes you should know
- Overhang mode: colours the areas that need support before you generate them. Use it every time before adding supports.
- WireFrame: shows the polygon mesh of the model — useful for spotting geometry problems.
- Normals mode: detects inverted normals that can cause problems when slicing.
- Flip Camera: simulates the real print orientation (platform on top, resin below). What you see is exactly what your machine prints.
- Picture View: 2D view of each sliced layer — the level of detail the LCD screen actually sees.
- Slice View: 3D layer-by-layer view of the sliced model. Drag the slider and look for islands and weak areas.
Full workflow: from the 3D model to the print file
This is the process we follow at 3Dwork. The steps are in order of dependency — skipping one or changing the order causes 80% of the problems we see in the community.
Step 1 — Import and orient the model
Drag your STL, OBJ, 3MF or LYS/LYT file directly into the viewport. Orientation is the most important decision in the whole process — a bad orientation can ruin a perfectly modelled part.
- Turn on Overhang mode before orienting — you will see in real time which areas hang in the air.
- Tilt the model 30–45° relative to the platform to reduce the maximum contact area per layer.
- Place the surfaces with the most detail facing up — layers formed away from the FEP are better defined.
- Avoid flat surfaces parallel to the platform — they create a huge suction cup when peeling and can tear the part off.
- The Auto-Orient button is a good starting point, but always check it by hand — the algorithm does not know which surface matters most to you.
Step 2 — The Magic Button (and when not to use it)

Lychee has the Magic button — one click that does automatic orientation + automatic supports + hollowing (if enabled). It is tempting, but you need to know when to use it:
- When it is fine to use it: quick prototypes, parts where orientation and support marks do not matter, a first pass to see whether the part is printable.
- When NOT to use it: miniatures with visible faces, jewellery, parts with critical surfaces, or when you want to control where the supports go.
- The Magic Button uses the preset supports active — before using it, make sure the right preset is selected (Light for fine details, Medium/Heavy for large parts).
Step 3 — Configure the supports

Lychee Plus’s Auto-Supports are the software’s biggest differentiator. The v7.5 ML algorithm analyses the model in three dimensions and sorts the areas into categories: flat overhangs, angled overhangs, floating islands, fine detail areas. For each category it applies a different strategy.

| Support type | When to use it | Key parameters |
|---|---|---|
| Auto-Support (ML) | Organic models, figures, complex parts | Light/Medium/Heavy preset depending on size |
| Manual | Spot fixes, critical areas the auto does not cover | Tip: 0.2–0.4 mm; Mid: 0.8–1.2 mm |
| Support Painting | Large surfaces with continuous overhangs | Medium-high density, long brush strokes |
| Projection Support | Flat or mechanical surfaces with regular geometry | Grid spacing: 1–2 mm |
| Grid Support | Wide bases or high-density rafts | Spacing 2–4 mm |
Step 4 — Hollow and suction cup detection

For large, solid parts, hollowing them can save a 50–70% of resin. Go to Tools → Hollow.
- Wall thickness: 1.5–2 mm for decorative figures; 2–4 mm for functional parts.
- Add at least 2 drain holes — one at the bottom (so the resin can drain while printing) and one at the top (to vent).
- Minimum hole diameter: 3–4 mm for standard resins; 5–6 mm for dense resins.
- Use the Interior/Exterior view to check that no closed cavities remain.
- The 3D Drain Holes Verification tool (Plus) checks in real time whether the holes are well placed before slicing.

Step 5 — Slicing parameters
The Settings panel is where you decide the quality and reliability of the print. See the full parameter section below.
Step 6 — Anti-aliasing
The parameters we use at 3Dwork: Smooth Surfaces on, radius 2 px, grey offset 40%. This setting smooths the edges between pixels without blurring fine detail, although depending on the XY resolution and the layer height you use, it is often advisable simply to leave it off.
Step 7 — Slice, review and export
Click Slice. Time varies from 10 seconds to several minutes depending on size and your hardware. When it finishes, two complementary views appear:
- Picture View (2D): what the LCD screen actually sees on each layer — the most faithful representation. Go layer by layer looking for islands (areas with no contact with the layer below).
- Slice View (3D): volumetric view of the sliced model. Useful for checking the overall structure of the supports.
- Use the Simulator to watch the print layer by layer, animated — you spot risk areas visually much faster.
- Once you are satisfied, Save to export in your printer’s format (.ctb, .goo, .photon, etc.) or send it directly over WiFi if your printer is on the same network.
Slicing parameters: the definitive guide
This is where prints are won or lost. Every parameter matters. We explain what each one does and the starting values we use at 3Dwork… but again, this is a suggestion to introduce you to what these settings are for. Ideally you experiment and learn to use them for your own machine, resin, printing conditions and preferences.
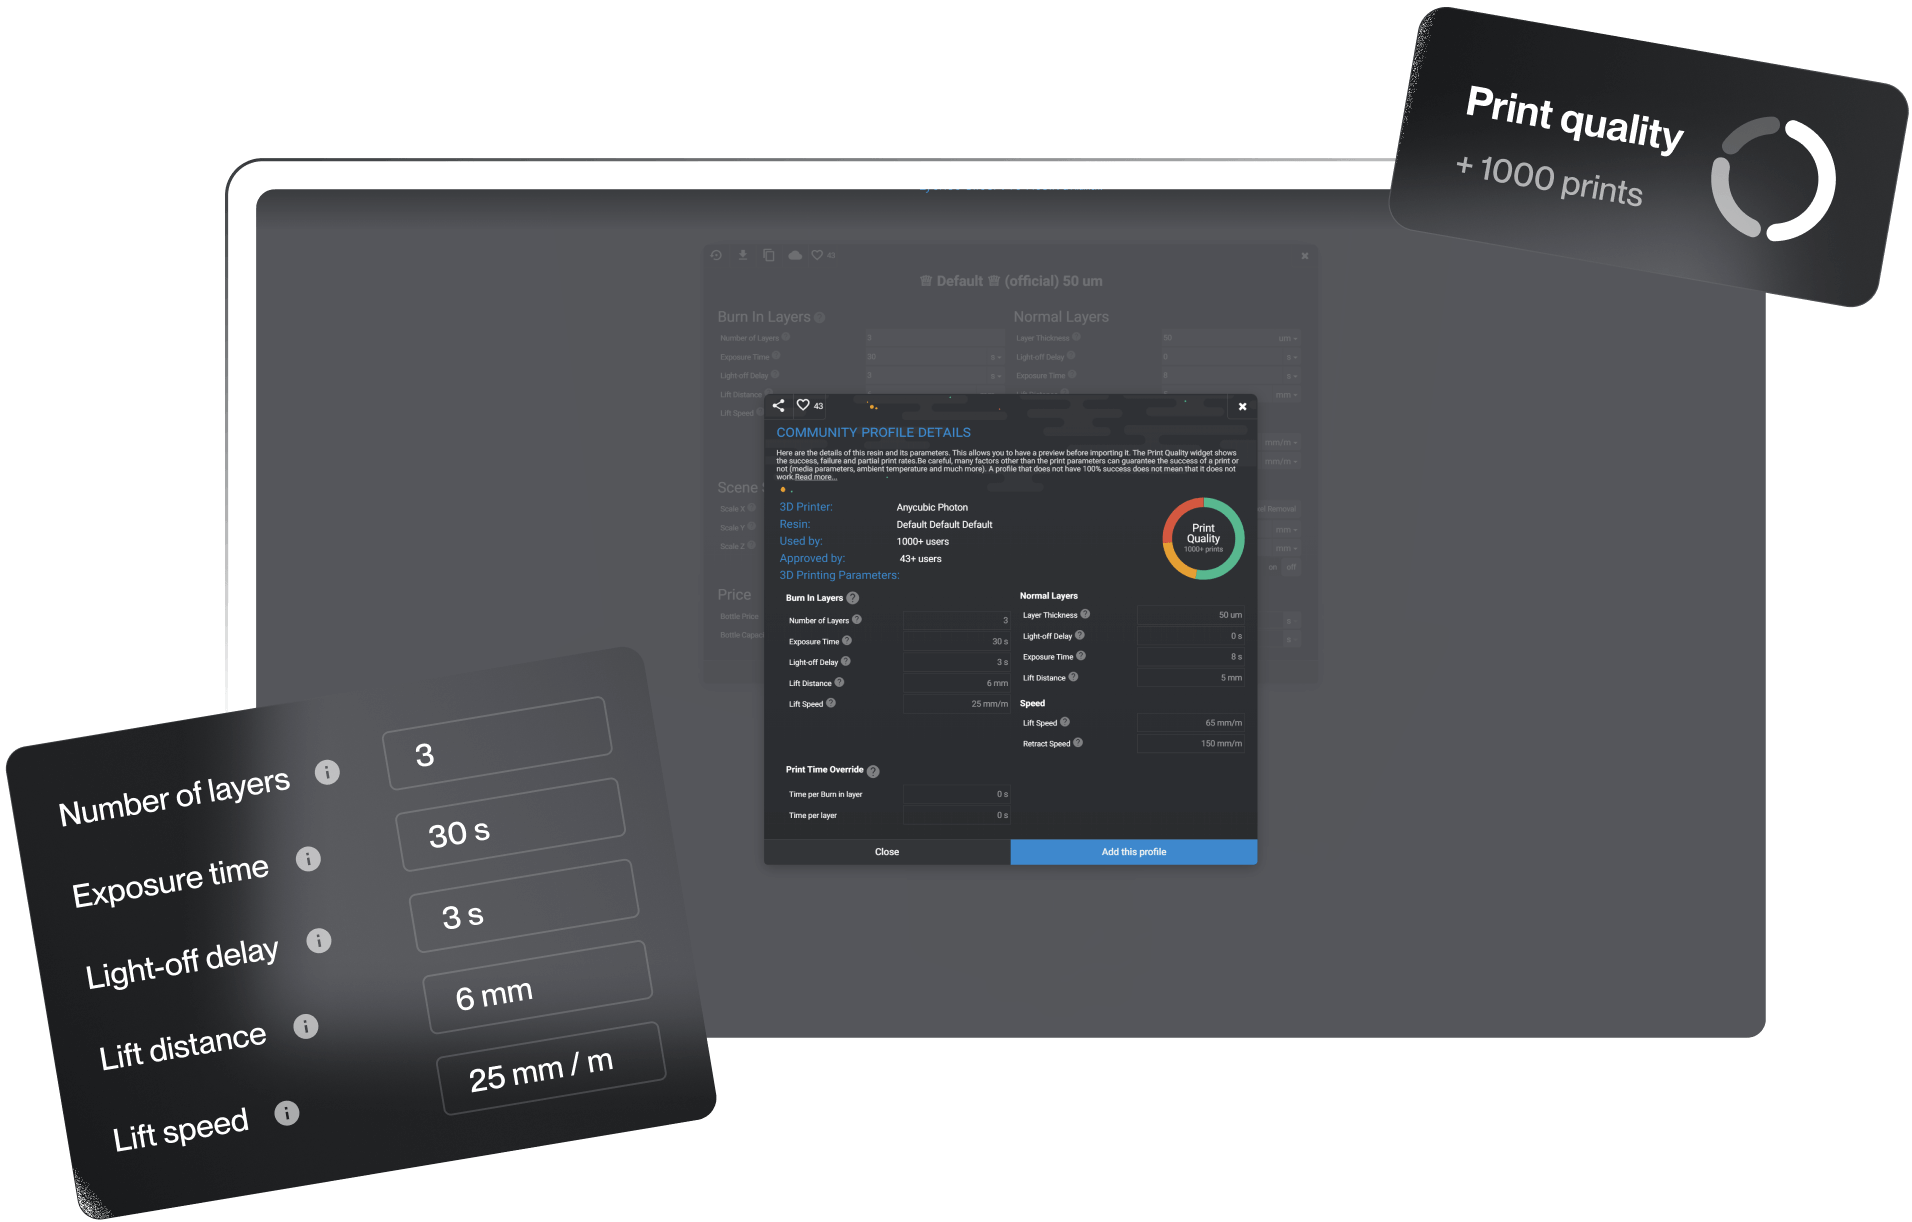
Something we love, as a reference point, is the community profiles section, where we can look up other users’ values for our machine/resin/layer height, which always helps.
Layer height / thickness
Resin and filament printers work in a very simple way… they deposit material layer by layer to build the object. In resin printing, layer height mainly affects the final quality on one side and the print time on the other.

Another important point to choose our optimal layer height is to look at our machine’s pixel size and, since what we are after is the best definition, use a layer height that gives us a voxel as square as possible. For example, if our machine has a pixel size of 29 µm, the optimal layer height is 30 µm (0.03).
As a rule of thumb, we will tell you that the human eye supposedly cannot tell the difference below 0.02 layer height, so if you want to play with this parameter, it is normally best not to go below 0.03.
Finally, also we must take into account the quality and design of the object to print. A figure without good resolution in its design or without fine details probably does not justify a low layer height, because we will gain nothing from it.
| Thickness | Ideal use | Relative time |
|---|---|---|
| 0.02 mm | Display quality: display pieces, macro photography | Very slow — only for extreme cases |
| 0.03 mm | Maximum detail: miniatures, jewellery, dental parts | Slow — ~3× compared with 0.05 |
| 0.05 mm | Standard — the best quality/speed balance | Reference |
| 0.08 mm | Quick prototypes, functional parts without fine detail | Faster |
| 0.10 mm | Maximum speed — noticeably lower quality | ~2× faster |
Burn-in layers (base layers)
In Lychee they are called burn-in layers (not “bottom layers”). These are the first overexposed layers that guarantee adhesion to the platform.

- Recommended number: 4 layers. From the 4th–5th burn-in layer onward, adding more does not improve adhesion — the part is already well stuck. What it does do is increase wear on the LCD screen, which has to withstand the high exposure times for more layers. More than 6 burn-in layers is counterproductive: more wear, same results.
- Burn-in exposure time: 25–40 s for small-to-medium parts; up to 40 s for large parts.
- Too low → the part does not stick.
- Too high → elephant foot (expansion in the first layers).
- Lift distance for burn-in: 25% more than for normal layers (e.g. if you use 4+4 mm normally, use 5+4 mm for burn-in).
- Lift speed for burn-in: never exceed 40 mm/min. Too fast on these layers can tear the part off.
Transition layers
Lychee has a very useful feature, and one that many people don’t know about, which some printers have by default in their firmware or can adapt intelligently: transition layers.

Basically these transition layers gradually adapt the exposure time between the base layers, which are usually long, and the normal layers, to avoid adhesion problems between layers or, sometimes, artefacts in the form of lines.
The number of these layers depends on each case, but a sensible number is usually to divide the base-layer exposure time by X until you get a value close to the time used on the normal layers.
Example: we have a base-layer time of 35 s and 2 s on the normal layers… 35 s / X = 2 approx… 35 /17= 2.05 -> we would use 17 transition layers.
Normal layers
If the previous layers were critical for the part’s adhesion to the build plate, these ones are important for giving the part consistency as it is built and for getting good detail definition on our figures.
The trickiest parameter to calibrate. It varies with the resin, the screen model and the layer thickness:
| Screen type | Typical range (0.05 mm) | Starting point |
|---|---|---|
| Monochrome 4K (35 µm) | 2.0–3.0 s | 2.5 s |
| Monochrome 6K–8K (20–28 µm) | 1.8–2.8 s | 2.0 s |
| Monochrome 12K–16K (16–22 µm) | 1.5–2.5 s | 1.8 s |
| RGB (models before 2021) | 7–12 s | 9 s |
- Signs of under-exposure: layers that separate, holes in solid areas, fragile parts, supports that break when removed.
- Signs of over-exposure: loss of detail in holes and slots, part dimensionally larger than expected, fine details that disappear.
The values in the table are only a starting point. The right time for your combination of printer, resin and temperature can only be found with an exposure test — there is no universal value. See the calibration section below.
Light-Off Delay (LOD)
The LOD is the time the printer waits from switching off the UV light until the platform moves down for the next layer. It gives the resin time to flow and settle.

- Starting point: 2 seconds for 10″ printers with standard resins.
- 3–4 seconds for large printers (13″+) or very viscous resins.
- Never set the LOD below 2 seconds — layer failures increase.
TSMC (Two-Stage Motion Control)
TSMC uses two speeds in the lift cycle: very slow in the first millimetres (to peel the layer without a sudden force) and fast for the rest (so no time is wasted).
- First stage: 40–45 mm/min, distance 3–4 mm. Gentle peel from the FEP.
- Second stage: 150–250 mm/min, distance 4–6 mm. Fast lift to the return point.
- Retract (down): 200 mm/min is safe; 60 mm/min for the last stretch before touching the resin.
- If your printer has a tilt mechanism (Saturn 4 Ultra, Mars 5 Ultra), turn on the TSMC toggle for tilt — the algorithm changes to suit that movement.
In the next image you can see exactly how the TSMC cycle works and the difference in behaviour between the two stages:

Calibration: the exposure test is mandatory
Community profiles are an excellent starting point, but you have to do the final calibration yourself, with your printer, your resin and your working temperature. One hour of calibration saves you dozens of print failures.

| Test | What it measures | Recommended setup |
|---|---|---|
| MCC Test (J3D-Tech) | Exposure + lift parameters in a single test — the most complete | 4 base layers, 3 transition layers, 2 s rest time — download on Cults3D |
| J3D Boxes | Dimensional tolerances — nested cubes 4/6/8 mm, checked with calipers | Free — download on Cults3D |
| Cone Test (TFF v3) | Exposure time using a cone geometry | 3 s starting point on mono; 9 s on RGB |
| RERF (Anycubic) | 8-exposure matrix in a single print | Included in Anycubic firmware — the most convenient if you have an Anycubic |
Lychee vs CHITUBOX: comparison
We have used both for years at 3Dwork. This is our unfiltered opinion, knowing that we are Lychee partners — that does not stop us from being fair:
| Criterion | Lychee Slicer | CHITUBOX |
|---|---|---|
| Base price | Free (Lite) | Free (Basic) |
| Auto-Supports | ✅ Advanced ML (Plus) | ✅ Basic (Basic) / Magic (Pro) |
| Suction Cup Detector | ✅ Plus | ❌ |
| 3D drain hole verification | ✅ Plus | ❌ |
| Community resin profiles | ✅ on all tiers | ❌ |
| FDM support | ✅ | ❌ (resin only) |
| Printer compatibility | 750+ models | 200+ models |
| UX / learning curve | Very intuitive | A bit more technical |
| Discord / Community | 29,000+ active members | Forums, more scattered |
| Pro/Plus price | €9.99/month | €15.99/month |
Conclusion: for most users who print resin regularly, Lychee Plus beats CHITUBOX Pro on price and on exclusive tools. CHITUBOX has more history and more documentation on forums.
Lychee has improved and, for us right now, it is the reference in this kind of slicer… if you are starting from scratch, start with Lychee.
Common failures and how to fix them
Nothing prints and there are no residues in the VAT

Sometimes we send a print and there is nothing on our build platform or in the VAT. We suggest checking:
- Check the screen, remove the VAT and build platform and run the screen test that printers usually include. If yours does not have one, with the VAT and platform removed and the screen protected with a sheet of paper, we run a test print. We check that the image displays correctly and that the UV power is right. If the screen or the UV shows problems, check whether your printer has a UV power adjustment and that it is not set wrongly. If not, the UV source may need replacing.
- Check the USB, it is advisable not to use the USB stick that usually comes with the printer. In any case, if we have the problem described, we try another USB. Remember that printers normally support USB drives in FAT32 format with partitions of 8–16 GB and USB 2.0.
- Check the state of the resin, if the above worked correctly, another possible cause is the state of the resin. To check this, we can expose a few drops of resin to sunlight or a UV torch for a few seconds to see whether it solidifies.
print stays in the VAT/resin tank, does not stick to the platform

A fairly common failure is lack of adhesion on the first layers, so the print stays on the FEP or hangs partially, which affects the finish of the part:

Example of total lack of adhesion on the first layers
- Incorrect levelling of our build platform, redo it following the manufacturer’s instructions. If it always fails on one side or one corner, that is also usually a sign of poor levelling.

- Damaged or defective build platform, sometimes the platform is not completely flat. With a reliable ruler and a light, we can check that our platform is in good condition.

- Lack of adhesion to the build platform, build platforms today come with laser-etched patterns to improve adhesion. If yours do not have them, we can roughen the surface a little with a nylon scouring pad. It is also advisable to clean the surface well with IPA between prints.
- Temperature, as we have already said, temperature and printing conditions are very important, so make sure the resin temperature is at least >20 ºC.
- Adjust the exposure of the first layers by raising it between 2 and 5 seconds to check whether it improves, the time for these is usually 6–10 times the value of the normal layers. It is important to stress that the time and number of these first layers can significantly reduce the useful life of the optical part.
- Other times, because of the stress of the printing process itself, the supports and bases can give way. In these cases
- Check that the FEP is well tensioned and in good condition
- Apply a layer of PTFE lubricant to our FEP to reduce stress
- Check the slicing: aspects such as part angle, hollowing, drain holes placed correctly…
- Set the lift and retract speeds below 40 mm/min, or through tests try lower speeds in 5 mm/min steps for the base layers
The base layers do not stick to the normal layers

Although it is not a very common failure, sometimes our base layers do not stick to the normal layers, as in the following images:

Only the base layers stick

The base layers do not stick to the normal layers.
This kind of problem is usually caused by an abrupt change in exposure time between the base layers and the normal layers, or because the normal layers use a very low exposure time.

In these cases it is important to keep in mind:
- make sure our base layers are between 6 and 10
- turn on transition layers, usually with the same number as the base layers

- set the lift and retract speeds below 40 mm/min, or through tests try lower speeds in 5 mm/min steps for the base layers
- increase the exposure time of the normal layers by 20%
- Adjust the light-off delay for our machine. You have a calculator with recommended times here
- Check the state of the VAT film (FEP, nFEP, PFA, ACF) that it is not slack or damaged
Only the supports print, the rest stays on the VAT film

Another very common failure is that our objects stay totally or partly on the VAT film, while the bases and supports stay stuck to our platform:

This problem usually happens because the supports are not strong enough to keep the object anchored.
There are several things to check in this case:
- Adjustments in the resin profile:
- Increase the exposure time by 10%
- reduce the retract and re-entry speed to 40 mm/min or less
- Adjust the light-off delay for our machine. You have a calculator with recommended times here
- Adjust the support options in your slicer:
- Increase the support density and the tip diameter
- avoid placing supports on flat surfaces; rotate the model to avoid them
- avoid model placement angles that can cause deformation from FEP tension, make sure to hollow parts whenever possible, be generous, and place the drain holes correctly
- For hollowing, make sure you do not use less than 1.5 mm; for large prints at least 2 mm; and have at least 2 drain holes of 3 mm at the bottom of the part
Vertical lines or gaps along the whole Z axis

If our prints come out with vertical lines or columns, or with holes all over the part along the Z axis.
- Check the screen, remove the VAT and build platform and run the screen test that printers usually include. If yours does not have one, with the VAT and platform removed and the screen protected with a sheet of paper, we run a test print. We check that the image displays correctly.
If the image on the screen is not correct, we check whether it is a dead pixel (which would leave a line or column of resin in our prints) or resin residue (which would leave holes in our parts).
In the first case, a dead pixel, the ideal is to replace the screen or avoid using that area to print. For resin residue on the screen, we check for possible VAT leaks and remove the resin residue with great care: apply a little IPA for a few seconds and wipe with a microfibre cloth. A plastic glass-ceramic scraper can also help, used with extreme care. There can also be occasional screen faults that leave some areas of the print cured and others not; in these cases we check the condition of the screen and its connections. - Check the USB, it is advisable not to use the USB stick that usually comes with the printer. In any case, if we have the problem described, we try another USB. Remember that printers normally support USB drives in FAT32 format with partitions of 8–16 GB and USB 2.0.
- Check the slicing, sometimes we see gaps or resin columns, or even a thin layer covering all or part of the print surface, in prints related to poor slicing. These can appear at random places depending on the model. We can run the screen test explained earlier to find the faults, or use the UVtools analyser.
Horizontal lines in our parts

Sometimes completely horizontal lines appear on our prints, which can originate from:
- A mechanical problem from wear or lack of maintenance on the Z axis. These usually appear with a pattern and at the same heights.
- Sudden temperature changes during printing can produce lines or bands on our parts, for example opening the lid or pausing the print.
- The condition of the film can also affect it, causing horizontal lines or bands in certain areas of our prints.
Parts stick too much to the platform

We do not consider this really bad, but sometimes very severe adhesion to the build platform can damage the platform or the model when it is removed.
- One way to avoid damaging the parts is not to remove them from the platform until after curing. We do the pre-wash/washes with the parts still on the platform, remove the supports with the help of a dryer on the platform itself, and once the parts are off we cure them. This gives us fewer chances to damage our parts when removing the leftover base and supports. A dryer can also make this task easier, along with a spatula or a plastic scraper.
- We can adjust the exposure of the base layers by reducing 5 s in each test to find a balance between low adhesion (the parts do not stick) and high adhesion (the parts are hard to remove).
For more troubleshooting reference, the excellent documentation of Lychee by our fellow J3D-Tech or the one from Ameralabs can be a great help.
Compatible printers and our reviews
Lychee is compatible with more than 750 resin printers. These are the ones we have analysed in depth at 3Dwork and with which we have validated the settings in this guide:
Anycubic
- Anycubic Photon P1 — dual VAT, 14K, Wave Release, the most innovative of 2026
- Anycubic Photon Mono 4 Ultra — 10K, 7″ monochrome screen
- Anycubic Photon Mono M7 Pro — built-in heater, high speed
- Anycubic Photon Mono M7 Max — huge volume (298×164×300 mm)
Elegoo
- Elegoo Saturn 4 Ultra 16K — the best large-format MSLA available
- Elegoo Saturn 4 — speed, precision and compact reliability
- Elegoo Mars 5 Ultra — the best budget MSLA of 2025

Frequently asked questions
Is Lychee Lite really free?
Yes, completely free. It includes basic slicing, manual supports, island detection, anti-aliasing and community resin profiles. The only paid features are the ML Auto-Supports, the Suction Cup Detector, the advanced 3D Hollow and full multiplate.
What is the difference between Lychee 7 and earlier versions?
Lychee 8 replaces Electron with its own engine. According to the manufacturer, preparing files uses 22 times fewer resources than in 7, and manual supports are placed 8.4 times faster (manufacturer figures, identical scenes). The 7 series brought the ML Auto-Supports 3.0 in v7.5. If you have a 5.x version or earlier, the difference in speed and support quality is huge.
Are community resin profiles reliable?
The most downloaded profiles with the most positive ratings are very reliable as a starting point. Use them to get 80% of the work done, then adjust with an exposure test for the remaining 20%. Do not mistake a community profile for the “final setting” — every printer has its small differences.
Can I use Lychee with my Anycubic/Elegoo/Creality printer?
Yes. All the main brands are supported: Anycubic (all Photon series), Elegoo (Mars, Saturn), Creality (HALOT, MAGE, RAY), Phrozen, Flashforge, NOVA3D, Voxelab and many more. See the full list at docs.mango3d.io.
What about the 30-day free Plus trial?
When you install Lychee for the first time or with a new account, a 30-day free Plus trial with all features activates automatically. You do not need a credit card. Use it to try the Auto-Supports, the Suction Cup Detector and the 3D Hollow.
Does Cloud Slicing work?
Yes, for Plus subscribers. Cloud slicing sends the model to Mango3D’s servers so the slicing runs there. It is useful for very complex models that crash the local PC. The result is identical to local slicing.
How do I update Lychee?
Lychee updates automatically. On startup, if a new version is available, it notifies you with a banner. Click “Update” and it downloads and installs without losing your profiles or projects. On Linux (AppImage) you have to download the new AppImage manually.


